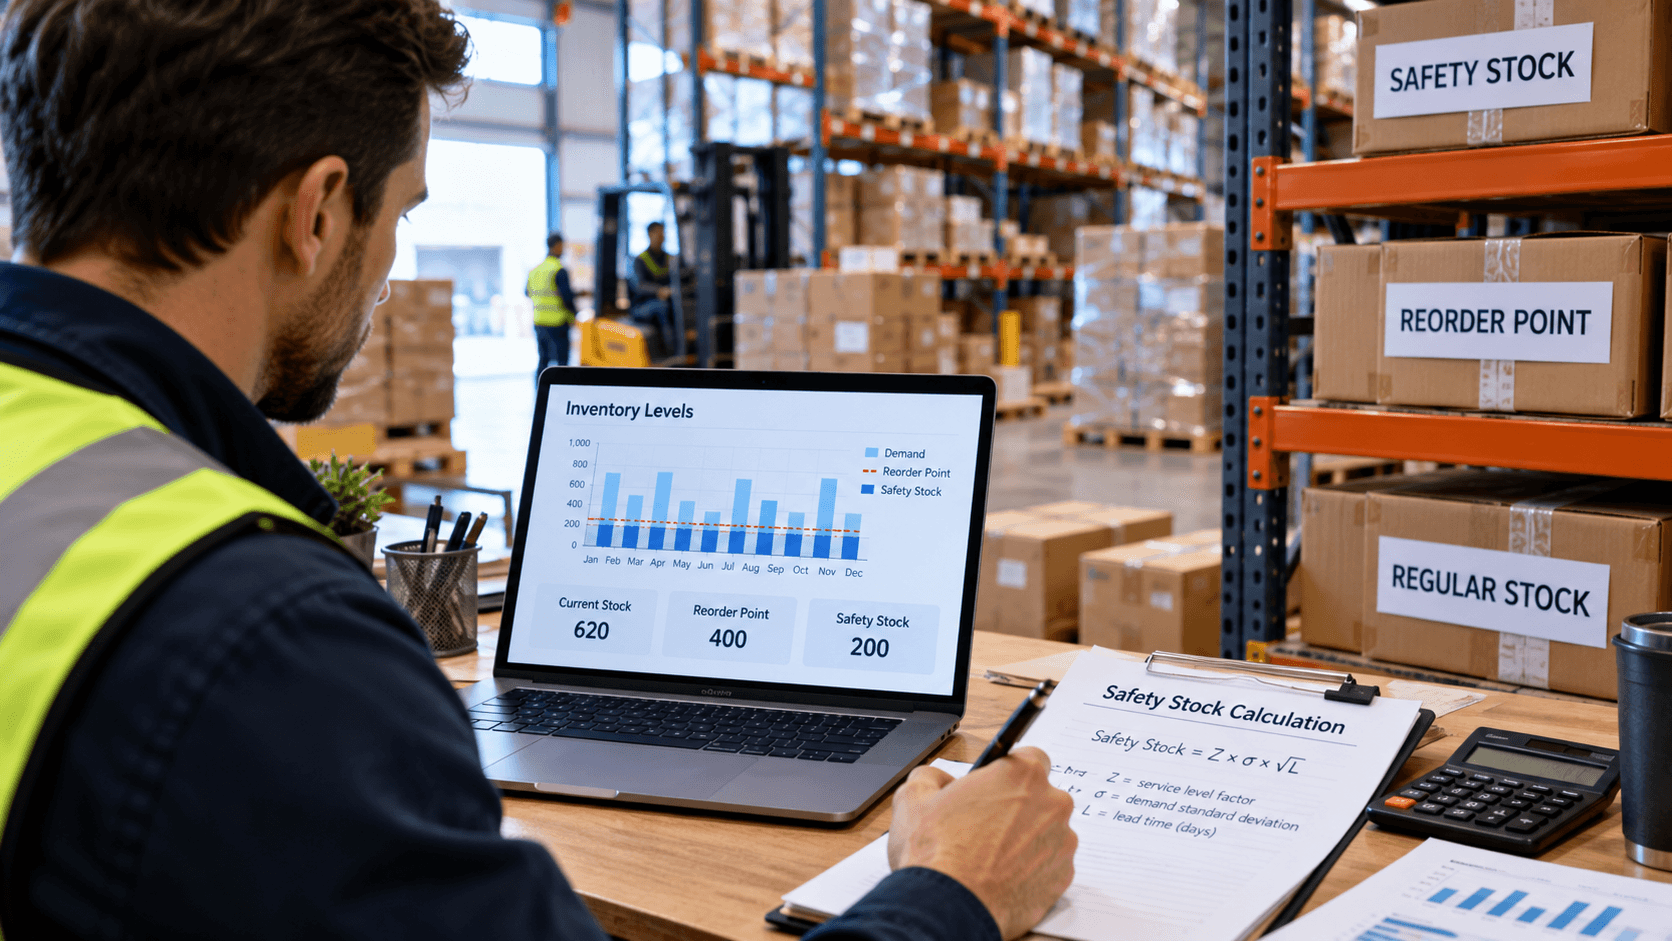
Safety stock is extra inventory held to reduce the risk of running out of products when demand is higher than expected or replenishment takes longer than planned. It acts as a protective buffer between normal inventory requirements and unexpected changes in supply or customer orders. The correct amount depends on demand variability, lead-time uncertainty, service-level targets, and the cost of holding stock.
Safety stock is important for wholesalers, retailers, manufacturers, and distribution centers because inventory shortages can interrupt customer operations. A distributor may forecast consistent weekly demand but suddenly receive a large customer order, experience a supplier delay, or face transportation disruptions. Without an appropriate inventory buffer, the business may miss sales, incur emergency shipping expenses, or damage customer relationships.
However, safety stock is not free. Additional inventory occupies warehouse space, requires financing, and may eventually become damaged, obsolete, or unsaleable. Effective inventory planning must therefore balance protection against stockouts with the financial burden of carrying additional merchandise.
What Is Safety Stock in Inventory Management?
Safety stock in inventory management is inventory held beyond expected demand during the replenishment period. Its purpose is to protect against uncertainty rather than cover ordinary sales that have already been forecast. Businesses often establish separate safety stock quantities for individual SKUs, locations, or product categories.
For example, a regional distributor may sell approximately 100 units of an industrial component each week. If replenishment normally takes two weeks, expected lead-time demand is 200 units. The distributor might hold an additional 50 units as safety stock to reduce the risk of running out during unexpected demand increases or supplier delays.
The 50-unit quantity is not automatically the correct level. It should be supported by historical demand, lead-time variability, business priorities, and the consequences of a stockout. A critical industrial component may justify a larger buffer than a slow-moving accessory with easily available substitutes.
Why Is Safety Stock Important?
Safety stock helps maintain product availability when actual demand or supply conditions differ from normal forecasts. Even reliable suppliers can experience delays, and customer ordering patterns rarely remain completely constant. An appropriately sized buffer reduces the chance that these variations will interrupt fulfillment.
Safety stock is especially important for distributors with contractual service expectations or customers that rely on timely replenishment. Restaurants may need packaging before their next operating day, while repair companies may require replacement parts to finish customer jobs. In these cases, product unavailability can create consequences beyond a single missed sale.
The benefit must still be evaluated financially. Excessive buffers can increase inventory carrying costs and reduce available cash for faster-selling products. A distributor should therefore establish safety stock policies according to measured supply uncertainty and customer-service requirements rather than applying one universal quantity to every SKU.
How to Calculate Safety Stock
Safety stock can be calculated using a simple maximum-demand formula or a statistical method based on demand variability, lead-time uncertainty, and a target service level. The most appropriate method depends on the quality of available data and how variable the supply chain is. Simple formulas are useful for initial estimates, while statistical models provide more structured planning when their assumptions are appropriate.
There is no universal safety stock formula that guarantees a specific fill rate. Businesses must understand what each method measures and whether its assumptions reflect actual operations. Historical data should be reviewed for promotions, seasonal demand, shortages, and one-time disruptions before calculating a buffer.
Safety Stock Formula Using Maximum Demand and Lead Time
The maximum-demand safety stock formula estimates a buffer by comparing a high-demand, long-lead-time scenario with normal expected demand. It is easy to calculate and may be useful for businesses with limited inventory data. However, the result depends heavily on how “maximum” demand and lead time are selected, and it does not correspond to a specific statistical service level.
Safety stock = (Maximum daily demand × Maximum lead time) − (Average daily demand × Average lead time)
All lead times should use the same time unit as demand. If demand is measured daily, lead time must also be measured in days. Using weekly demand with daily lead times without conversion produces incorrect results.
Step-by-Step Safety Stock Calculation
Suppose a wholesaler has the following operating data:
The calculation is:
Safety stock = (60 × 8) − (40 × 5)
Safety stock = 480 − 200
Safety stock = 280 units
Under this method, the business would establish a 280-unit buffer based on the selected maximum and average values. The estimate may be conservative if extreme demand and extreme lead time rarely occur together. Businesses should therefore compare the result with actual inventory carrying costs and historical stockout outcomes.
| Variable | Value |
|---|---|
| Average daily demand | 40 units |
| Maximum daily demand | 60 units |
| Average supplier lead time | 5 days |
| Maximum supplier lead time | 8 days |
Safety Stock Formula Using Standard Deviation
A statistical safety stock formula estimates the buffer required to achieve a selected probability of avoiding a stockout during replenishment lead time. It uses demand variability and a service-level factor rather than simply choosing maximum historical values. This approach is useful when demand history is sufficiently reliable and the statistical assumptions are reasonable.
When lead time is fixed and demand varies independently across periods, a commonly used formula is:
Safety stock = Z × σd × √L
Where:
- Z = service-level factor.
- σd = standard deviation of demand per period.
- L = replenishment lead time measured in the same periods.
The formula assumes that the demand variation across periods can be appropriately represented by the model. It is less suitable for strongly intermittent demand, correlated demand patterns, or major seasonal shifts without adjustment.
Statistical Safety Stock Example
Assume a distributor records an average daily demand of 50 units, a daily demand standard deviation of 12 units, and a fixed replenishment lead time of 9 days. Management chooses a 95% cycle service-level target, corresponding to a Z value of approximately 1.645 under a normal-demand approximation.
Safety stock = 1.645 × 12 × √9
Safety stock = 1.645 × 12 × 3
Safety stock ≈ 59 units
The distributor would use approximately 59 units as the modeled safety stock, before applying any practical rounding or packaging constraints. This quantity is much smaller than some maximum-based estimates because it is derived from statistical variation rather than a combination of extreme observations.
The result does not guarantee a 95% order fill rate. A cycle service level describes the probability of not stocking out during a replenishment cycle under the stated assumptions, while fill rate measures the portion of demand satisfied immediately from available stock. These metrics require different analyses.
Safety Stock Formula With Variable Lead Time
When both demand and supplier lead time vary, safety stock calculations must account for uncertainty in both variables. A distributor receiving products in four days on one order and twelve days on another faces a different exposure from a business with a fixed replenishment schedule. Ignoring lead-time variability can understate the required buffer.
One commonly used approximation, assuming independent daily demand and lead time and suitable underlying statistical conditions, is:
Safety stock = Z × √(L × σd² + d² × σL²)
Where:
- Z = chosen cycle service-level factor.
- L = average replenishment lead time.
- σd = standard deviation of daily demand.
- d = average daily demand.
- σL = standard deviation of replenishment lead time in days.
This formula is an approximation rather than a universally valid model. Demand autocorrelation, irregular lead-time distributions, seasonality, and relationships between demand and supplier performance may require more advanced analysis.
Variable Lead-Time Example
Assume average daily demand is 40 units with a standard deviation of 10 units. Average replenishment lead time is 5 days, with a lead-time standard deviation of 1.5 days. The target cycle service level is 95%, using Z = 1.645.
Safety stock = 1.645 × √(5 × 10² + 40² × 1.5²)
Safety stock = 1.645 × √(500 + 3,600)
Safety stock = 1.645 × √4,100
Safety stock ≈ 105 units
The result is approximately 105 units when rounded up to a whole item. Lead-time variability contributes substantially to the total buffer in this example. Improving supplier consistency could therefore reduce inventory requirements without sacrificing the target service level under the model.
Safety Stock Service Levels Explained
A safety stock service level expresses the desired reliability of inventory availability under a defined measurement method. Many statistical calculations use cycle service level, which concerns the probability that stock remains available throughout a replenishment cycle. Businesses should avoid treating cycle service level and unit fill rate as interchangeable.
Z values assume a one-sided standard-normal model.
Moving from 95% to 99% requires a materially larger Z value. The safety stock increase can be substantial, especially when demand or lead-time variability is high. Management should therefore consider the economic cost of stockouts and inventory holding when selecting service targets.
Critical items may justify higher levels than easily replaceable products. Similarly, high-margin products with predictable repeat demand may warrant different policies from obsolete-prone items. A service-level target should be a documented business decision rather than an arbitrary number entered into inventory software.
| Target cycle service level | Approximate Z value |
|---|---|
| 90% | 1.282 |
| 95% | 1.645 |
| 97% | 1.881 |
| 98% | 2.054 |
| 99% | 2.326 |
Safety Stock vs. Reorder Point
Safety stock is the protective inventory buffer, while the reorder point is the inventory-position threshold that triggers replenishment. The reorder point normally includes expected demand during supplier lead time plus safety stock. Confusing these concepts can cause a business to order too late or carry the wrong quantity.
For a simple continuous-review inventory system:
Reorder point = Average demand during lead time + Safety stock
When average demand is measured per day:
Reorder point = Average daily demand × Average lead time + Safety stock
Reorder Point Calculation Example
Suppose a distributor sells an average of 30 units per day. Supplier lead time averages 10 days, and the business has calculated 90 units of safety stock.
Expected lead-time demand = 30 × 10 = 300 units.
Reorder point = 300 + 90 = 390 units.
Under a continuous-review system, the business would typically place a replenishment order when inventory position falls to approximately 390 units. Inventory position generally includes on-hand stock plus outstanding replenishment orders minus backorders or other relevant commitments. Using only the visible quantity on warehouse shelves can cause incorrect order timing.
The reorder quantity itself is a separate decision. It can depend on economic order quantity, supplier MOQ, available purchasing budgets, transportation requirements, and forecast demand. The guide to Inventory Management for Distribution provides broader context for replenishment policies.
Safety Stock vs. Buffer Stock
Safety stock and buffer stock are often used interchangeably to describe inventory held against unexpected shortages. Some businesses use buffer stock more broadly for any inventory reserve maintained to stabilize operations. Definitions can vary between systems and organizations.
The critical requirement is internal consistency. Inventory policies should define what a buffer covers, how it is calculated, and who can authorize the use of reserved stock. Without consistent definitions, buyers and warehouse teams may interpret the same quantity differently.
Safety Stock vs. Cycle Stock
Cycle stock covers expected demand between replenishment orders, while safety stock protects against uncertainty. Cycle stock is the merchandise a business plans to consume through ordinary sales during an ordering cycle. Safety stock remains as additional protection when demand or replenishment deviates from expectations.
For example, a wholesaler ordering 500 units every ten business days may use most of those units to meet predictable demand. The extra reserve held beyond normal planned consumption is safety stock. Separating the two helps purchasing teams distinguish ordinary replenishment quantities from protective inventory.
How Much Safety Stock Should a Business Hold?
The appropriate safety stock quantity depends on demand variability, supplier reliability, replenishment lead time, and the business impact of shortages. There is no universal recommendation to hold exactly one week, two weeks, or a fixed percentage of sales. Such rules can be useful as preliminary heuristics but should not replace inventory analysis.
Products with stable demand and short, dependable replenishment lead times may require relatively small reserves. Products with volatile demand, unpredictable suppliers, or critical customer-service requirements may need higher buffers. Seasonal or rapidly changing products require special care because historical averages can be misleading.
Safety Stock by Inventory Category
These categories should not be treated as universal numeric rules. A small distributor may initially use a simple segmentation process, while a larger organization can integrate statistical models into ERP or inventory planning software. The goal is to apply the appropriate level of analysis to each product's operational importance.
| Inventory category | Planning consideration |
|---|---|
| High-volume, stable-demand SKU | Use reliable demand history and lead-time measures |
| High-volume, volatile SKU | Model demand variability carefully |
| Slow-moving SKU | Consider intermittent-demand methods and cash exposure |
| Critical replacement part | Evaluate stockout consequences and recovery time |
| Perishable product | Limit buffers based on shelf life and waste |
| Imported product | Account for long and uncertain replenishment lead times |
| Seasonal merchandise | Adjust forecasts and buffers across the season |
How to Reduce Safety Stock Without Increasing Stockouts
Safety stock can often be reduced by improving demand forecasts, shortening replenishment lead times, and making supplier performance more predictable. The objective is to reduce underlying uncertainty rather than merely lowering reserve quantities. Cutting buffers without addressing operational causes increases the risk of shortages.
Improve Demand Forecast Accuracy
Demand forecasting should incorporate recent sales, seasonality, promotions, significant customer changes, and known upcoming orders. Forecast accuracy should be measured by product category rather than judged from aggregate revenue alone. A forecast can appear accurate overall while missing demand for individual high-priority SKUs.
Reduce Supplier Lead-Time Variability
Supplier consistency can be as important as average delivery speed. A supplier delivering in seven days every time may be easier to manage than one averaging six days but occasionally taking three weeks. Monitoring delivery performance helps buyers estimate the uncertainty that safety stock must cover.
Use Alternative or Backup Suppliers
Qualified backup suppliers can reduce exposure to disruptions at a primary manufacturer. However, alternative sources must be evaluated for price, product equivalence, quality, and availability. A backup relationship that has never been tested may not perform reliably during a shortage.
Improve Inventory Data Quality
Inaccurate inventory records can make even a well-calculated safety stock policy ineffective. Inventory position should account for received goods, customer commitments, outstanding orders, and damaged or unavailable items. Regular cycle counting and consistent transaction recording improve replenishment decisions.
Review Minimum Order Quantities
Large supplier minimums can increase total inventory beyond the calculated safety stock requirement. This creates additional cash exposure even when the protective buffer itself is reasonable. The guide to Minimum Order Quantity explains how supplier minimums affect inventory planning and purchasing risk.
How to Calculate the Cost of Holding Safety Stock
The cost of holding safety stock can be estimated by multiplying the value of the buffer by an annual inventory carrying-cost rate. This gives a simplified estimate of the financial burden of maintaining additional stock. Actual costs vary by product, storage requirements, financing, insurance, deterioration, and obsolescence exposure.
Annual safety stock carrying cost = Safety stock units × Unit inventory cost × Annual carrying-cost rate
Assume a distributor carries 500 units of safety stock with an inventory cost of $20 per unit. If its estimated annual carrying-cost rate is 20%, the calculation is:
500 × $20 × 0.20 = $2,000 per year
The 20% rate is an illustrative planning assumption, not a universal benchmark. Businesses should estimate their own cost of capital, warehouse expenses, shrinkage, insurance, and relevant inventory risks. A high-value product with slow turnover may justify careful review of the cost of every additional reserve unit.
This calculation can be compared with the expected cost of stockouts. Missed gross profit, emergency freight, contractual penalties, and customer-service consequences may justify holding an additional buffer. When those costs are measurable, a cost-based inventory policy can complement service-level calculations.
Common Safety Stock Mistakes
Common safety stock mistakes include using outdated demand data, ignoring lead-time variation, confusing on-hand stock with inventory position, and applying the same rule to every SKU. Each error can create either excessive inventory or unexpected shortages. A dependable policy requires regular review of both forecasts and actual performance.
A particularly common mistake is using the highest demand ever recorded as if it represents normal purchasing needs. Another is calculating a statistically precise buffer from unreliable data or assuming that a 95% cycle service level means 95% of customer units will always be filled. The model must match the business process and the intended service metric.
Businesses should also review the stock policy whenever supplier terms, product demand, warehouse locations, or customer requirements change. Safety stock is not a quantity that should remain unchanged indefinitely. Recalculation is especially important after significant supply disruptions or changes in order patterns.
Final Takeaway
Safety stock protects a business against demand and replenishment uncertainty, but the correct buffer is a calculated business decision rather than a fixed percentage of inventory. Its purpose is to maintain reliable product availability without tying up more working capital than necessary. Simple formulas can provide preliminary estimates, while statistical models support more structured decisions when suitable data exists.
Distributors should evaluate safety stock alongside reorder points, supplier performance, inventory carrying costs, and customer-service targets. Improving demand forecasts and lead-time consistency can be as valuable as increasing inventory. The strongest safety stock policy protects important sales while keeping cash available for the products and opportunities that matter most.
ʼ
Frequently Asked Questions
- What is safety stock in simple terms?
- Safety stock is additional inventory held to protect against unexpected demand or supply delays. It reduces the risk of running out of products during replenishment. The appropriate quantity depends on uncertainty and service requirements.
- What is the basic safety stock formula?
- One basic method subtracts average lead-time demand from a selected maximum-demand and maximum-lead-time scenario. A common expression is (maximum daily demand × maximum lead time) − (average daily demand × average lead time). More advanced formulas use standard deviation and service-level targets.
- Is safety stock the same as reorder point?
- No. Safety stock is a reserve intended to protect against uncertainty, while the reorder point tells the business when replenishment should be triggered. A simple reorder point is expected demand during lead time plus safety stock.
- Can safety stock be zero?
- Yes, a business may choose zero safety stock when demand and replenishment are sufficiently predictable or when stockout consequences are acceptable. This decision requires understanding the risk of shortages. Zero safety stock does not mean the business should hold no cycle inventory.
- How often should safety stock be recalculated?
- Safety stock should be reviewed when demand patterns, lead times, supplier performance, or service targets materially change. Fast-moving or volatile products may need frequent reviews, while stable items may require less frequent recalculation. The appropriate schedule depends on business conditions.
- Does more safety stock guarantee fewer stockouts?
- More safety stock can reduce stockout risk under otherwise similar conditions, but it cannot guarantee uninterrupted availability. Extreme demand, supplier failures, inaccurate inventory records, and operational errors can still cause shortages. Additional stock also increases carrying costs.